Spiral Tower Conveyor

A spiral tower conveyor carries products up (or down) a continuous helical belt inside a vertical tower, packing tens or hundreds of meters of conveying length into a footprint of only a few square meters.

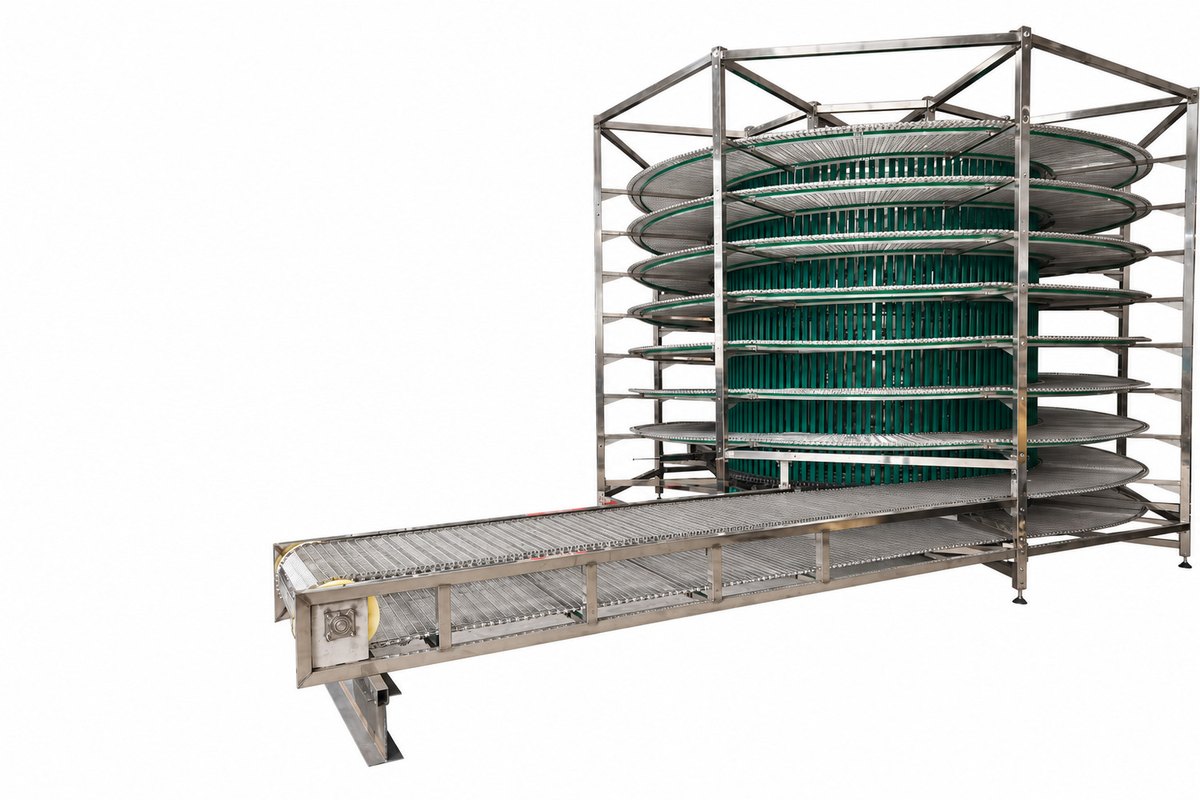
Reference illustration of Spiral Tower Conveyor

Product Overview

For biscuit and bakery plants, the Wanttone spiral tower conveyor is the space-efficient answer wherever extended in-line time is needed — ambient cooling of hot biscuits after the oven, product buffering and accumulation before packaging, or proofing, chilling, and freezing applications — keeping product moving continuously without manual transfer or large horizontal conveyor runs.

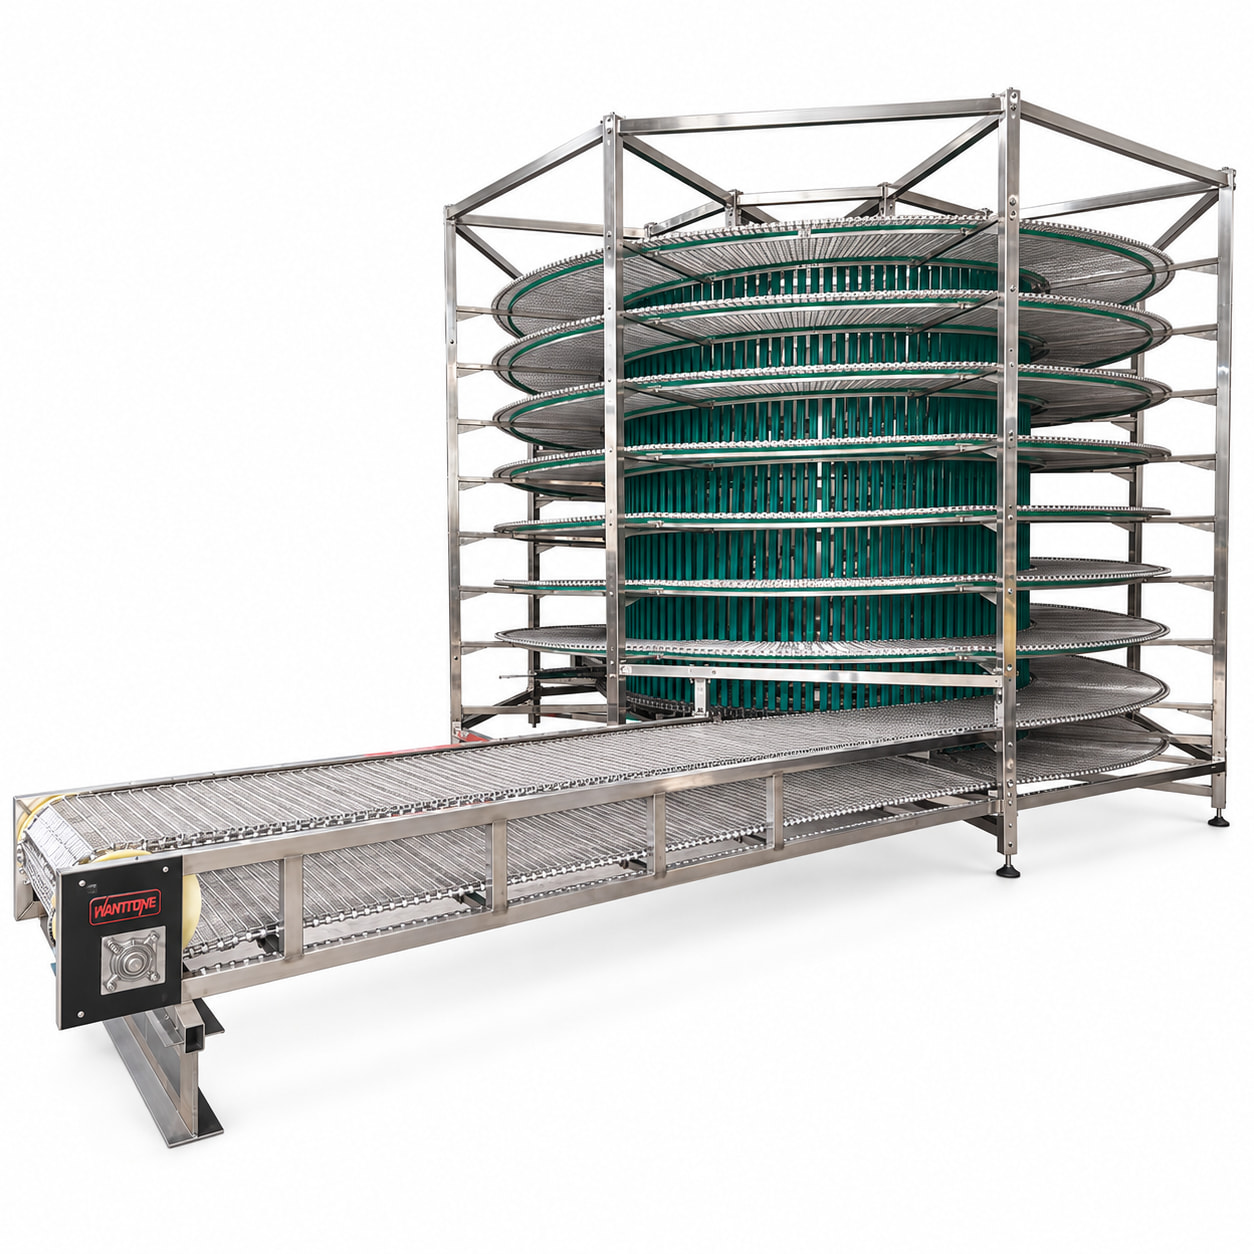
Original spiral conveyor with layered green belt guides and a horizontal discharge belt
Spiral conveyor and horizontal discharge section — original equipment view
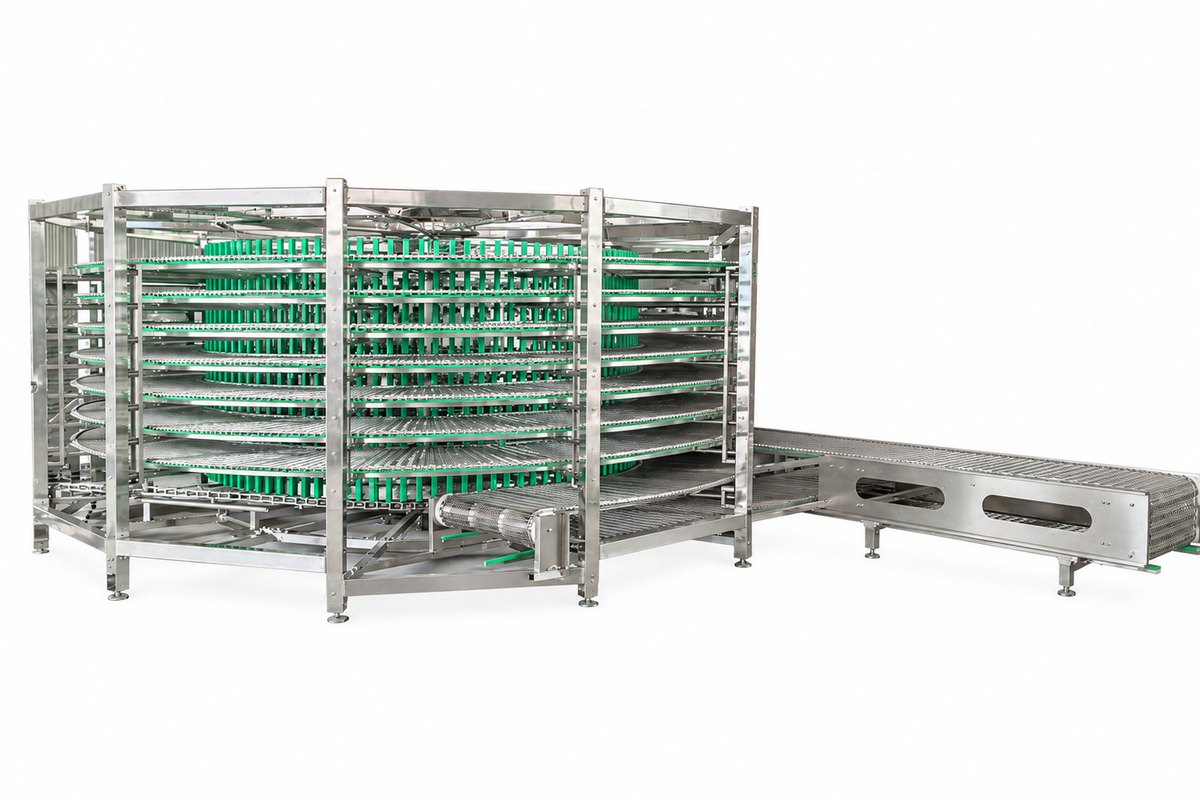
Original spiral cooling tower showing its cage, green belt guides and projecting conveyor
Spiral cooling tower and projecting conveyor — original equipment view

Capabilities & Applications

Key Features

  • Massive Cooling Length, Minimal Footprint

    The helical multi-tier design provides the long residence time biscuits need to cool to room temperature using a fraction of the floor space a straight cooling conveyor would require.

  • Continuous, Gentle Product Flow

    Products travel smoothly on a single continuous belt path with no transfers between sections, eliminating the jams, drops, and edge damage that transfer points cause.

  • Flexible Process Functions

    One tower platform serves ambient cooling, buffering/accumulation ahead of packaging, or integration into chilling and freezing zones, depending on your process design.

  • Configurable Tier Count & Direction

    The number of tiers, belt width, infeed height, rotation direction, and up-flow or down-flow routing are all configured to your capacity and plant layout.

  • Food-Grade Hygienic Construction

    Stainless-steel structure and food-grade belt materials with open access for cleaning meet modern bakery hygiene requirements.

  • Stable Drive & Speed Control

    Low-tension drum-drive design with frequency-conversion speed control synchronizes tower throughput with upstream oven output and downstream packaging.

Applications

  • Spiral tower conveyors are used wherever a biscuit or bakery line needs time: cooling hot biscuits, cookies, crackers, cakes, and Swiss rolls after baking; buffering product between processes to smooth out stoppages; and proofing or freezing in plants that combine baking with chilled or frozen products. They are particularly valuable in space-constrained factories and in high-capacity lines where horizontal cooling conveyors would simply be too long.

A Defined Role in the Line

  1. Upstream Requirements

    Confirm the incoming material or product condition, target throughput, infeed height and available utilities.

  2. Core Machine Function

    The helical multi-tier design provides the long residence time biscuits need to cool to room temperature using a fraction of the floor space a straight cooling conveyor would require.

  3. Downstream Integration

    Match discharge height, line speed, control signals, guarding and cleaning access with the next operation.

Specifications & Configuration

Technical Parameters for Spiral Tower Conveyor
ItemSpecification (typical range, customizable)
StructureVertical helical (spiral) tower, multi-tier
Belt width400–800 mm common (customizable)
Number of tiersConfigured to required residence time
Effective conveying lengthTens to hundreds of meters per tower
FunctionAmbient cooling / buffering / proofing / chilling / freezing
Belt typeFood-grade, low-tension spiral belt
FrameFood-grade stainless steel
DriveDrum drive with frequency-conversion speed regulation
Flow directionUp-flow or down-flow; clockwise or counter-clockwise

Every Wanttone spiral tower is engineered to order — share your product, capacity, and available space for a configured design.

The Wanttone Difference

Spiral towers are among the most engineering-intensive machines in a biscuit plant, and Wanttone builds on unusually deep foundations: a predecessor factory that has developed automated biscuit equipment since 1981, an in-house Foodstuff Machinery Research Institute, and whole-plant design as a core service. We calculate the residence time your product needs, then engineer tier count, belt speed, and tower placement around your building — the same way we engineered complete lines for demanding projects, including a fully automatic compressed biscuit production line developed for a Chinese military research program. ISO 9001 manufacturing, on-site installation and commissioning, operator training, and lifetime after-sales support come standard with every tower we deliver.

Frequently Asked Questions

When should I choose a spiral tower instead of a horizontal cooling conveyor?

Choose a spiral tower when your required cooling time demands a conveyor longer than your floor space allows, or when you need large buffering capacity. We assess both options during line design.

What products can run on the spiral tower?

Biscuits, cookies, crackers, cakes, Swiss rolls, and similar baked products. Belt specification and tier pitch are matched to product size and weight.

Can the tower do more than cooling?

Yes. The same platform can be configured for buffering and accumulation before packaging, or integrated into chilled or frozen zones for proofing, chilling, or freezing processes.

How is the required tower size calculated?

From your line capacity (pcs/min or kg/h) and the residence time your product needs. We then configure belt width, tier count, and speed to deliver that time within your available footprint.

Is the tower difficult to clean and maintain?

The open stainless-steel structure provides good access for cleaning, and the low-tension drive reduces belt wear. Routine maintenance is limited to cleaning, belt inspection, and drive lubrication, supported by our after-sales team.