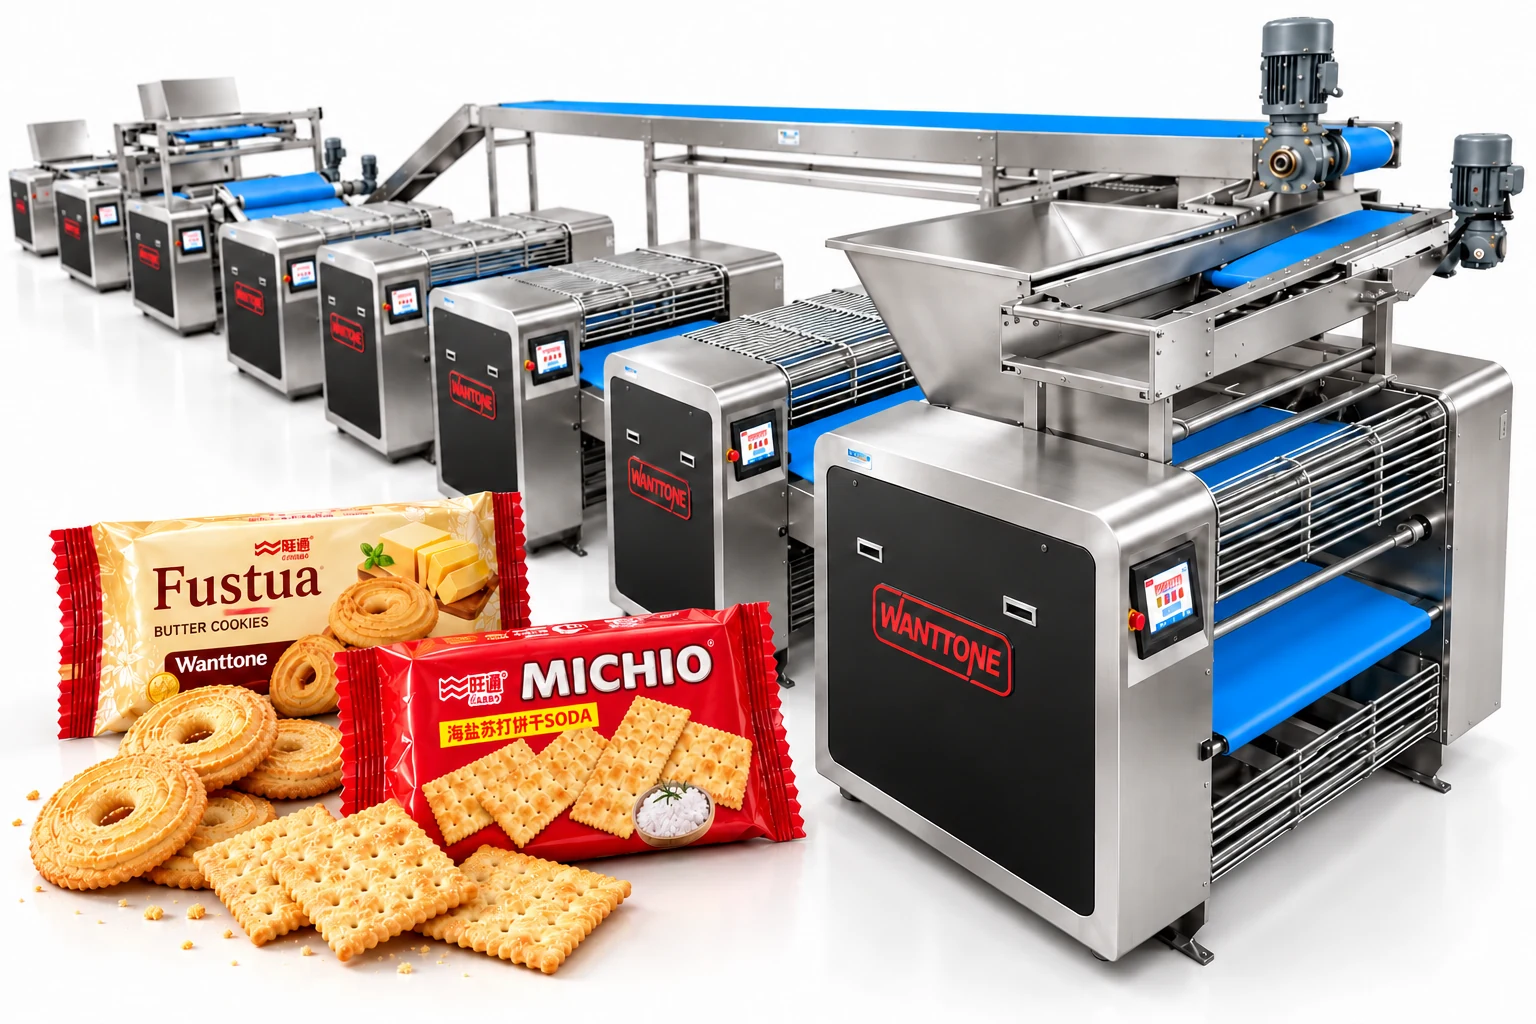
Machinery System
ISO 9001 structures equipment manufacturing, inspection, handling of nonconforming parts and corrective action.
Quality Control
Machinery quality follows an ISO 9001-controlled delivery process; food production follows ISO 22000 and HACCP controls through packing and dispatch.
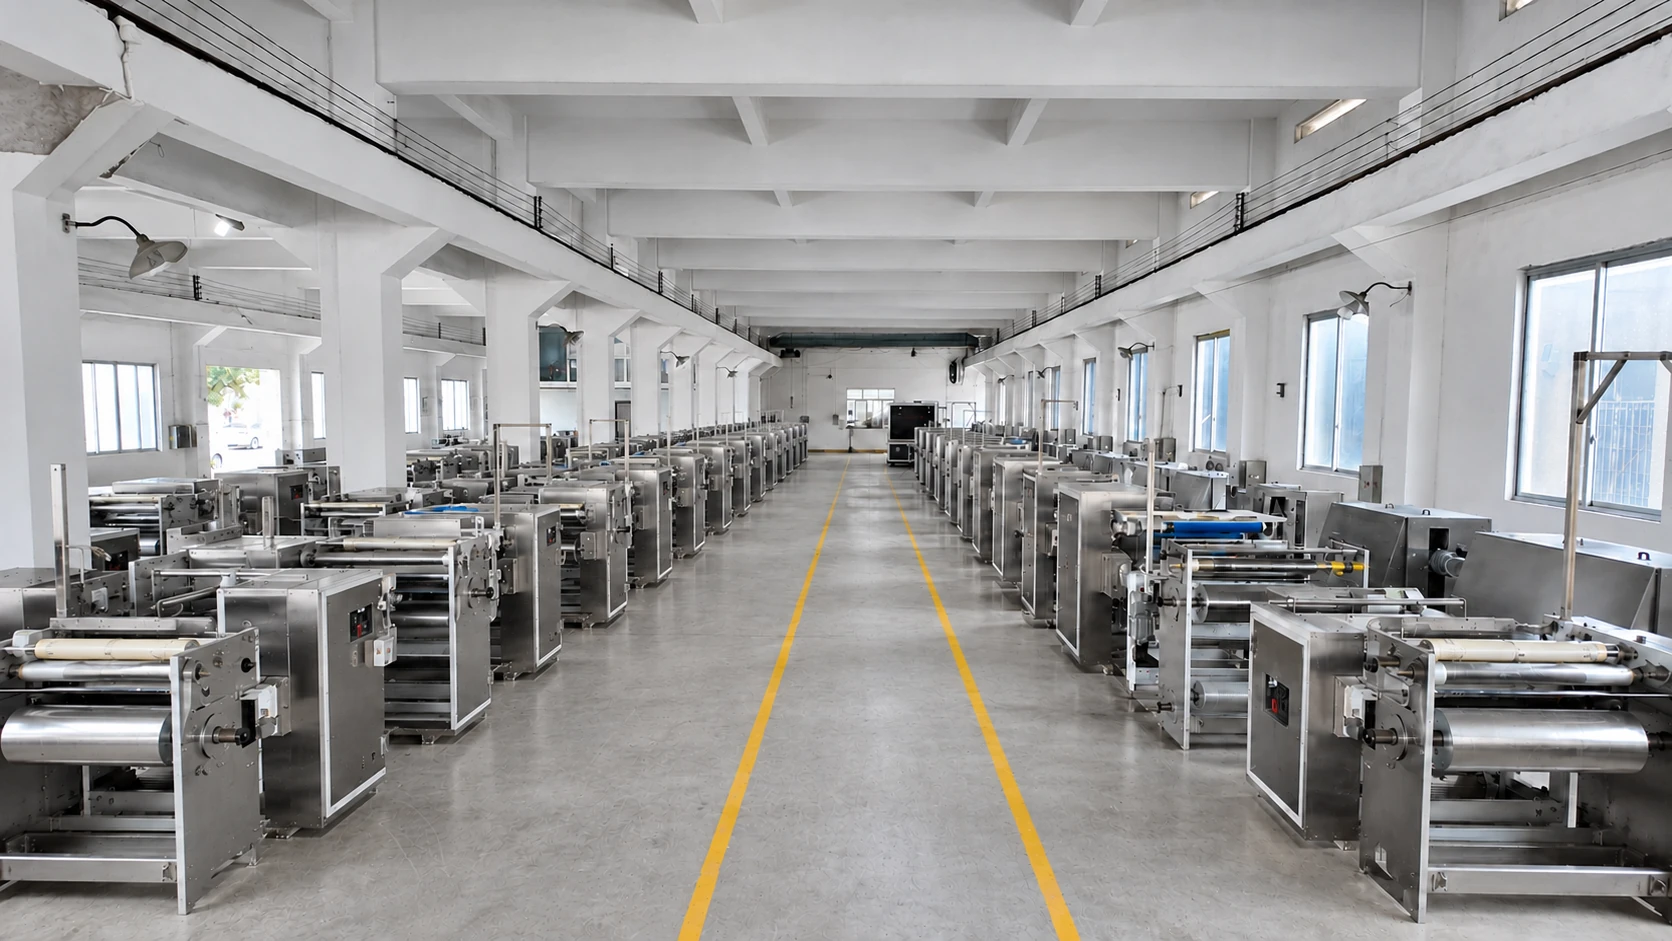
Control Structure
A machine must be built, inspected, tested and commissioned. A biscuit must move safely and consistently from raw material to finished pack. The two systems are connected, but they are not interchangeable.
ISO 9001 structures equipment manufacturing, inspection, handling of nonconforming parts and corrective action.
ISO 22000 and HACCP structure food-safety responsibilities and critical controls throughout commercial production.
Machinery Quality Flow
The machinery process is designed around the agreed line scope and closes only after operation, installation and handover have been addressed.
Materials and purchased components are checked before they enter assembly.
Fabrication, machining and assembly follow the confirmed equipment and line scope.
Completed equipment is inspected and tested against the agreed configuration before shipment.
Technician dispatch, installation, tuning and operator handover close the delivery loop.
Food Quality Flow
The food process combines recipe execution, time and temperature control, detection, packaging and release within the certified food operation.
Supplier and material checks begin the documented food process.
Recipes and batch conditions are controlled before forming.
Equipment settings shape the product to the confirmed specification.
Time and temperature control the bake and final product structure.
Controlled cooling protects texture before packing.
Metal detection and packaging controls protect the finished product.
Finished goods are stored and released through the export workflow.
Product Commitments
Product claims and project acceptance criteria are reviewed against the agreed recipe, pack, destination and inspection scope.
Available recipes are developed around a zero-trans-fat basis where confirmed for the selected product.
The stated shelf-life basis depends on the confirmed product, packaging, storage and distribution conditions.
Production records, packing and dispatch documentation support the agreed export route.
Match every certificate, shelf-life statement and customer reference to the exact product or equipment scope it documents.
Tell us what you have in mind. Share your questions or project requirements, and leave your contact details so our team can respond.
ricky@wanttone.com(86)13926311528Yangjiang, Guangdong, China